Quality Built into Every Step
From incoming materials and production processes to testing and final inspection, we apply systematic quality control throughout the entire manufacturing process.
Get in Touch
Integrated Capabilities for Reliable Manufacturing
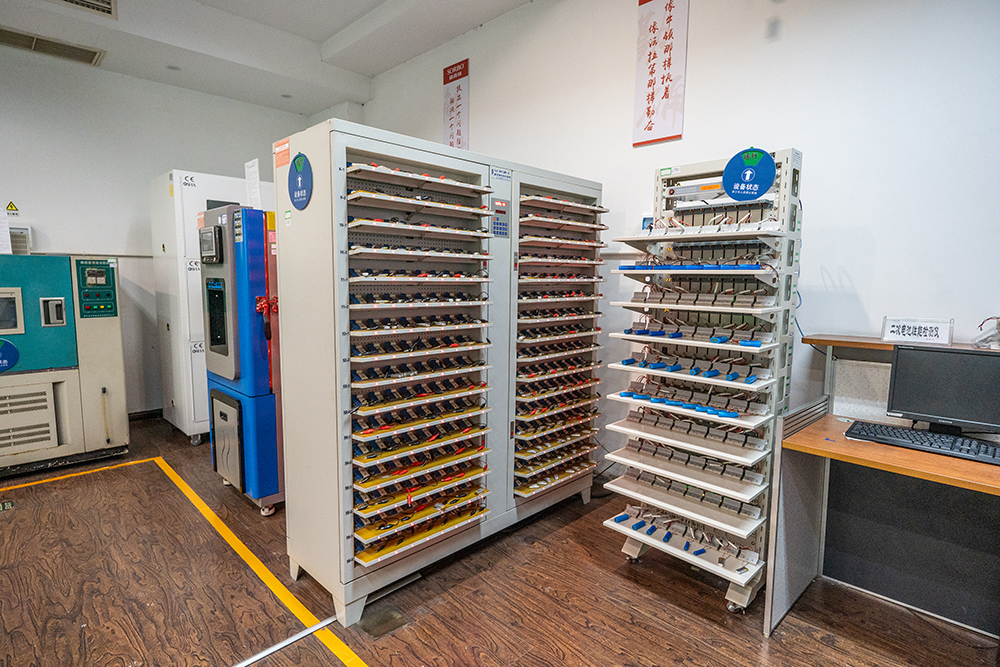
From R&D and quality control to in-house testing, SORBO integrates the expertise and resources needed to turn product concepts into reliable, production-ready solutions.
Quality Built Into Every Product
From incoming materials to final inspection, every product undergoes rigorous quality control and verification to ensure consistent performance, safety and reliability.
Quality First
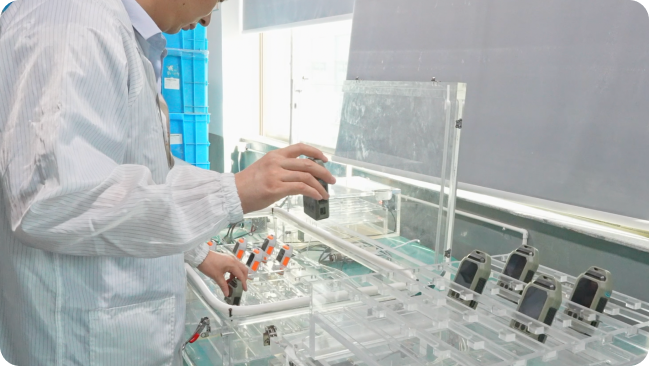
Quality is built into every stage of our process—from incoming material inspection and production control to testing and final verification—to ensure consistent product performance and reliability.
Customer Focus
We listen closely to customer requirements and market feedback, translating them into clear quality standards, product improvements and responsive support throughout each project.
Continuous Improvement
We continuously improve our products, processes and quality systems through testing data, production feedback, corrective actions and ongoing process optimization.
Global Compliance
Our quality management processes support applicable international standards and market requirements, helping customers meet product compliance needs across different regions and markets.
Quality System
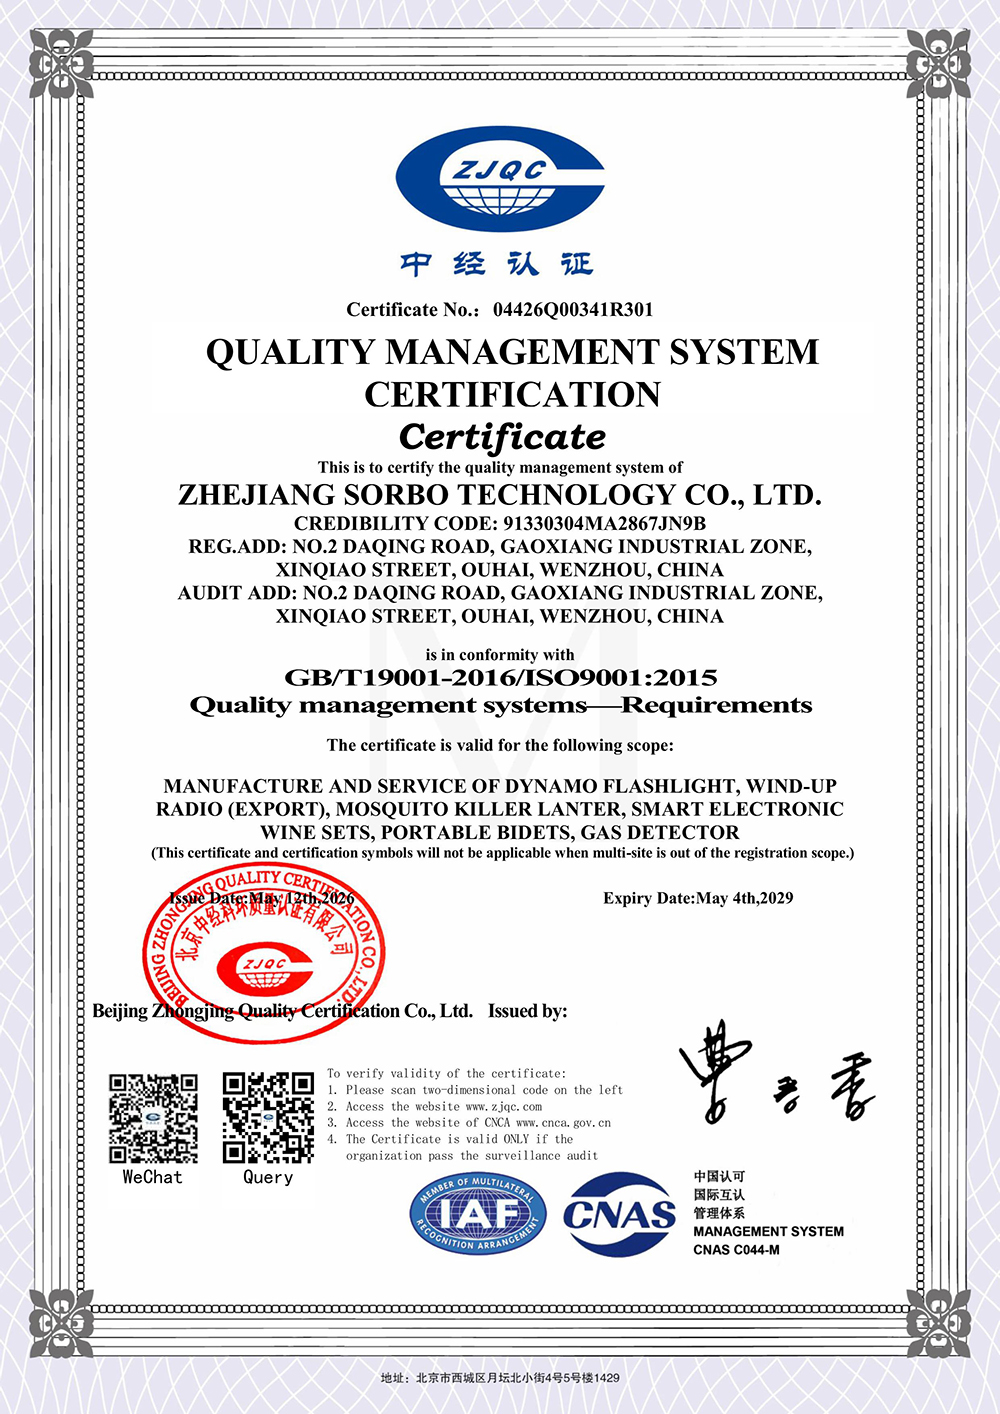
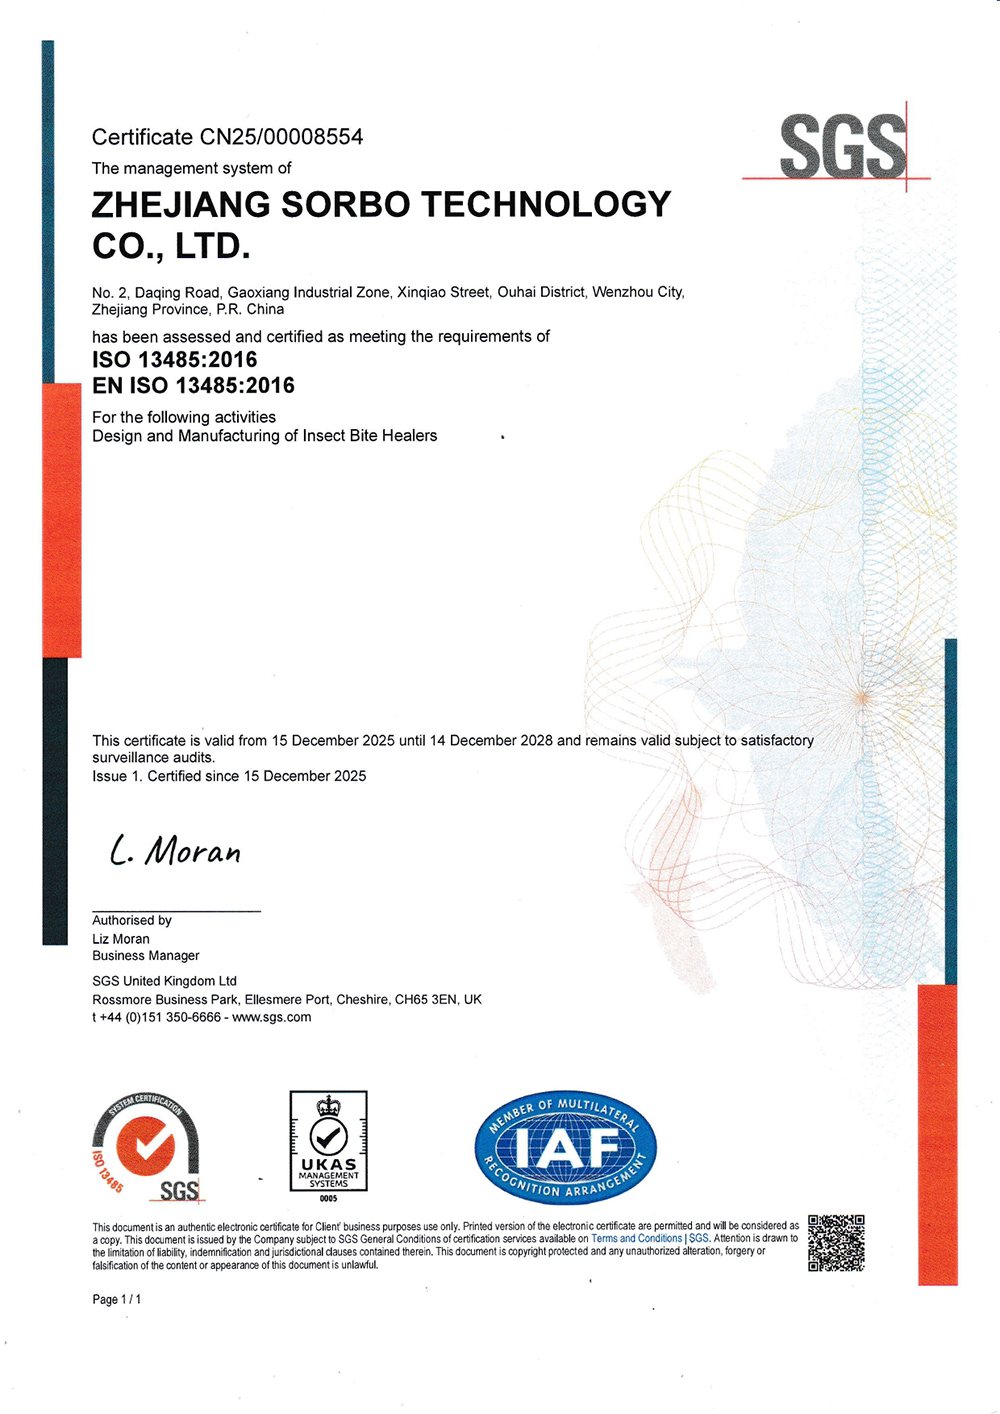
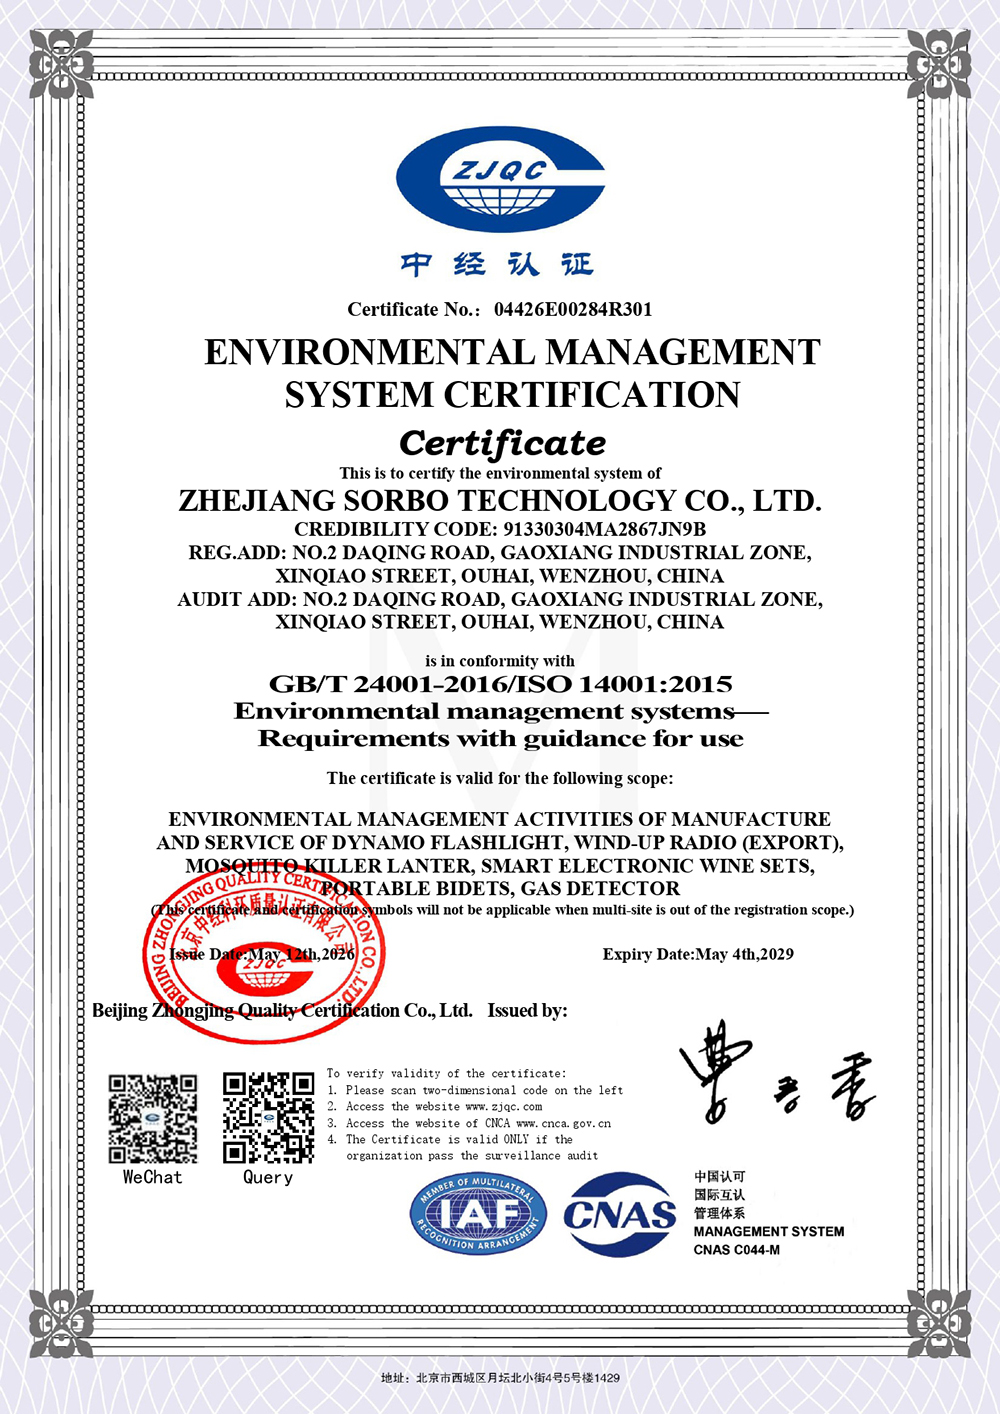
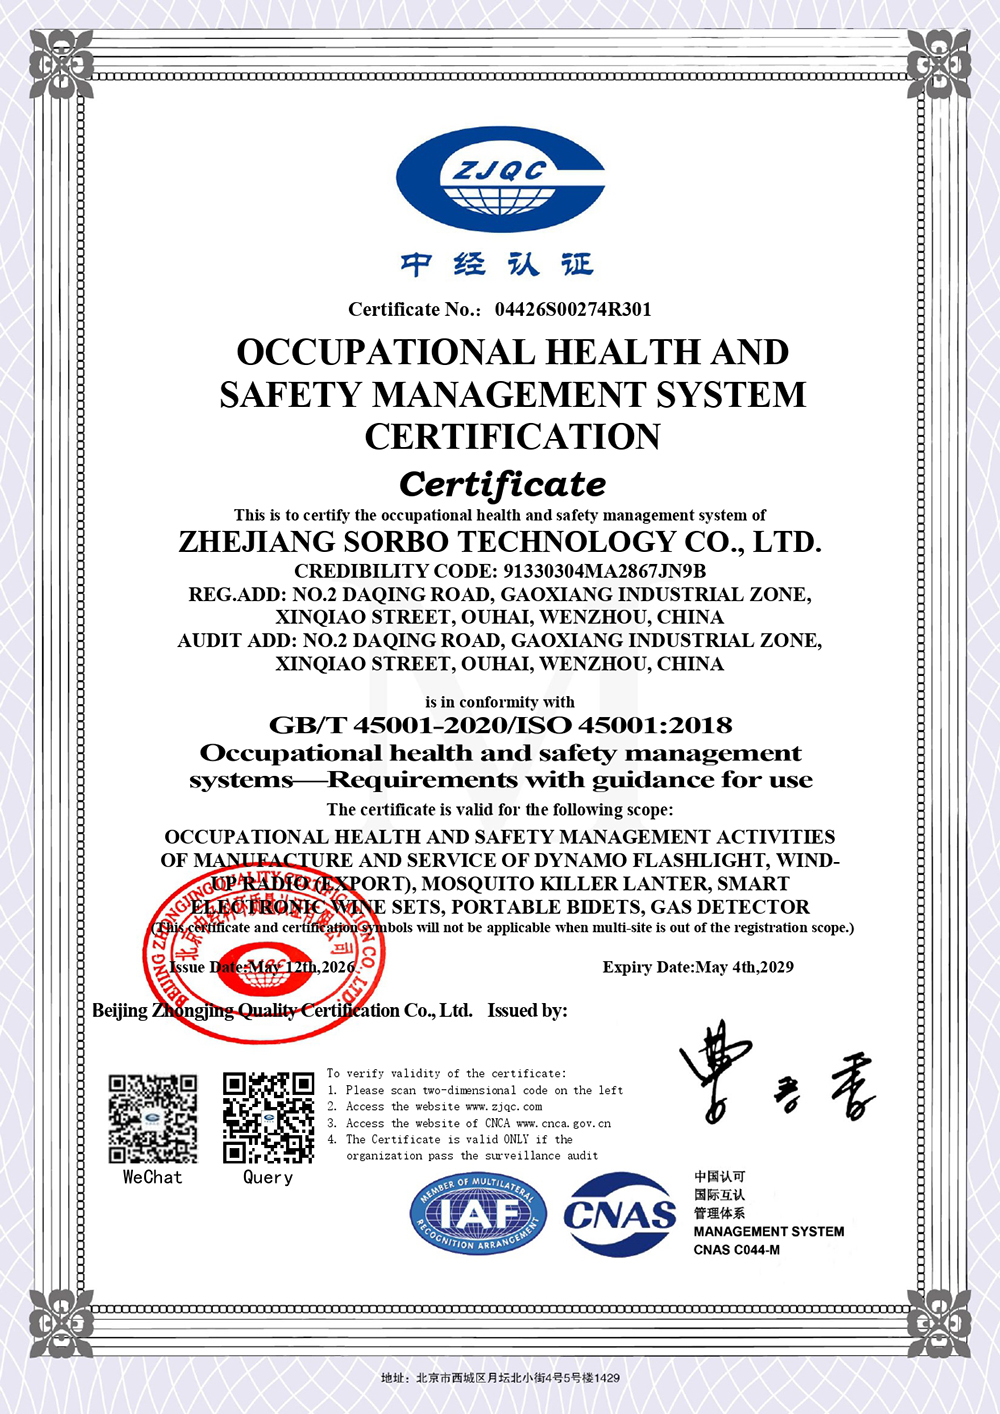
SORBO operates under certified management systems including ISO 9001:2015, ISO 14001:2015 and ISO 45001:2018, providing a structured foundation for quality, environmental responsibility and occupational health & safety.
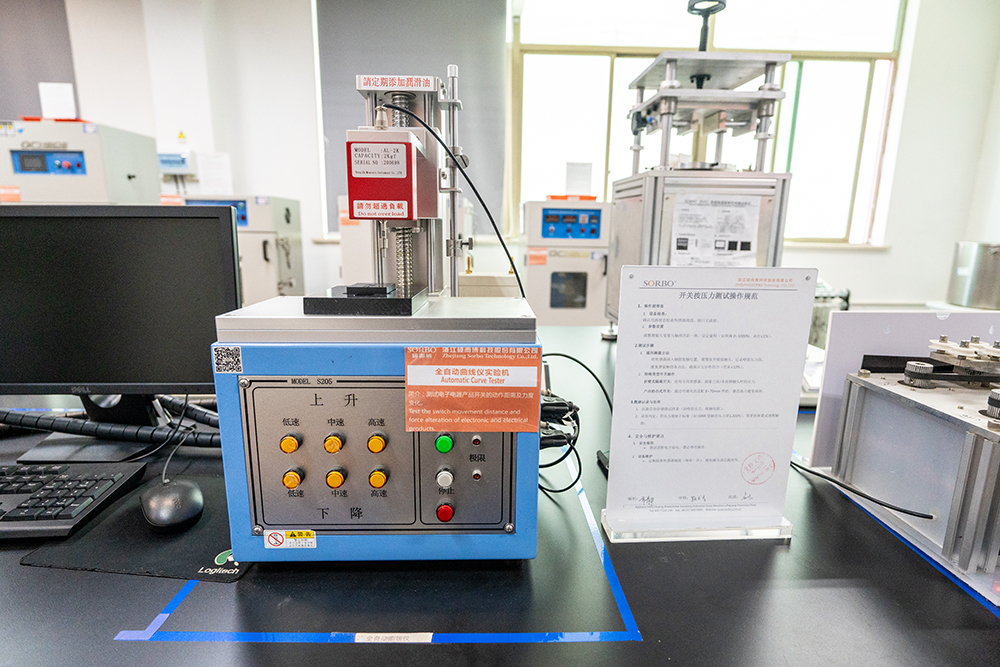
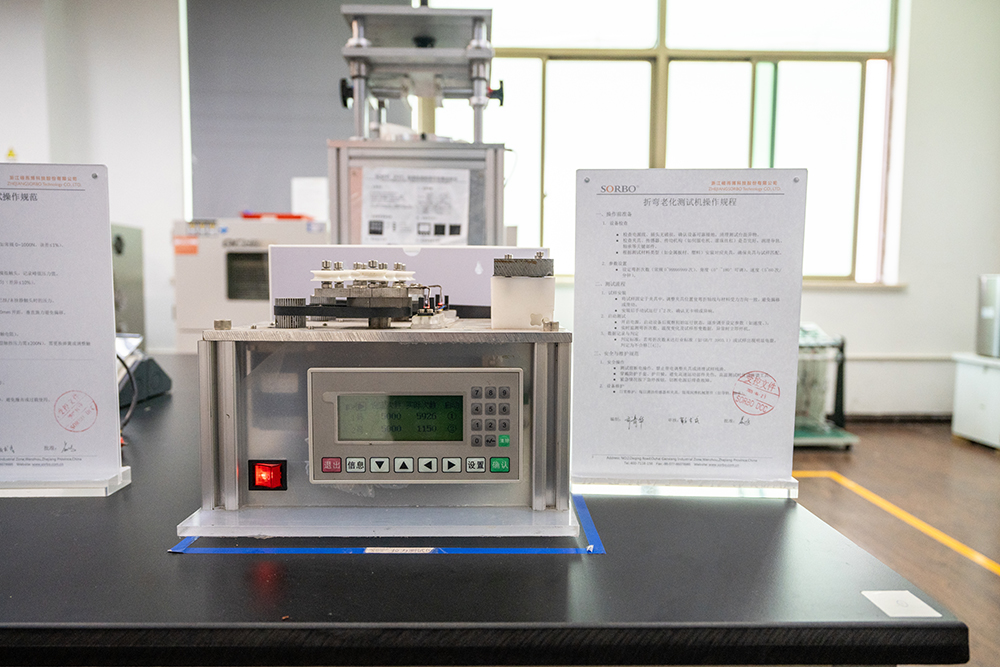
Our quality management covers incoming material inspection, in-process control, product testing, final inspection, traceability and continuous improvement to help ensure consistent quality throughout the entire manufacturing process.
Quality Control Process
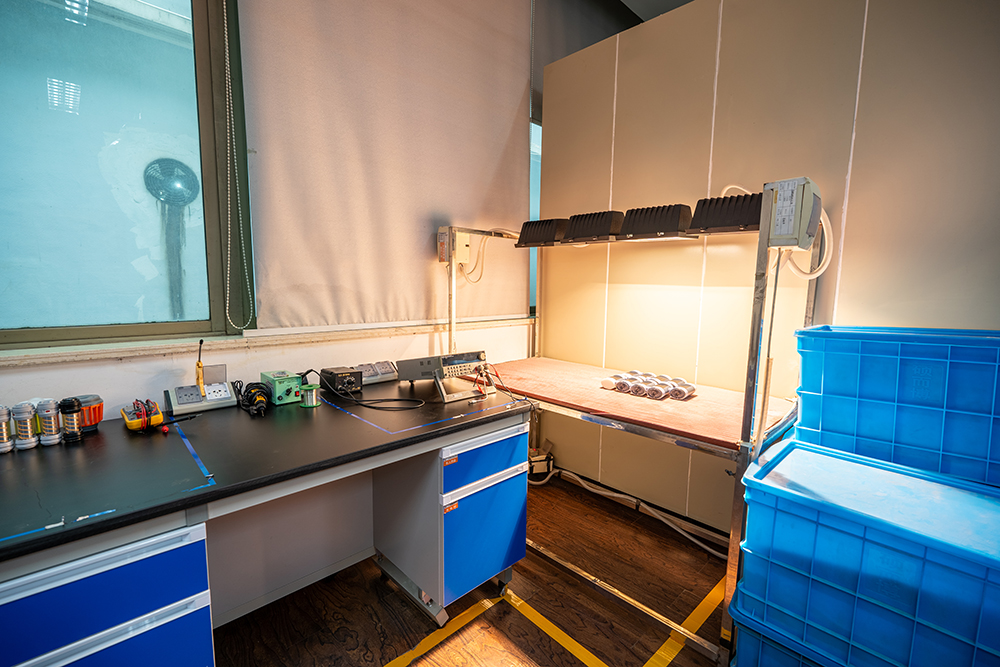
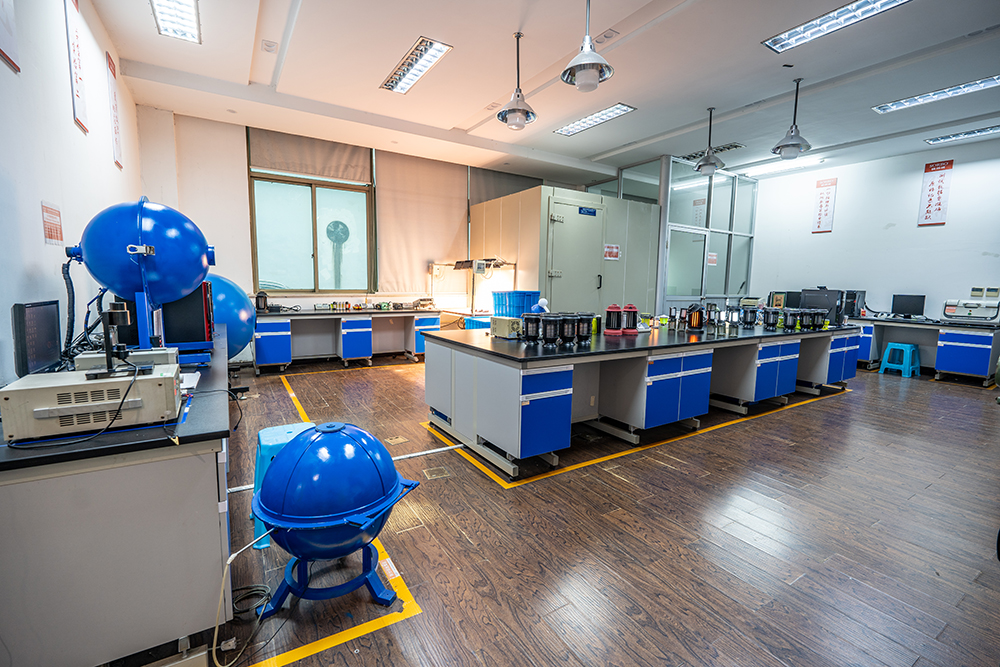
Quality is controlled throughout the entire manufacturing process—from incoming materials and production to testing, final inspection and shipment. Our structured quality control procedures help ensure consistent performance, reliability and compliance for every product.
- 1Incoming Material Inspection
- 2Supplier & Component Verification
- 3In-Process Quality Control
- 4Functional Testing
- 5Safety & Reliability Testing
- 6Final Product Inspection
- 7Outgoing Quality Control
- 8Traceability & Continuous Improvement
Product-Specific Testing
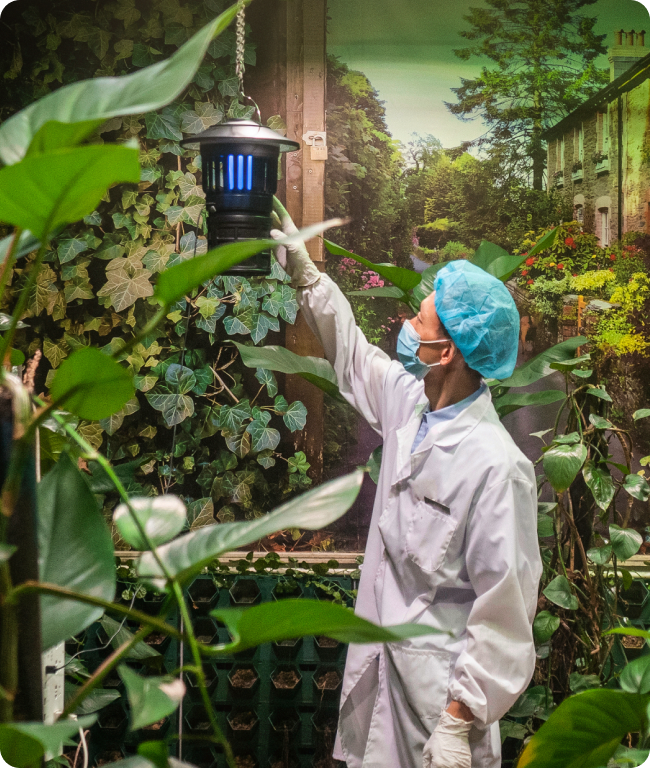
We apply dedicated testing procedures for each product category—from water flow and waterproof performance for portable bidets, to sensor response and alarm verification for gas detectors, and UV performance and trapping effectiveness for mosquito control products. Product-specific testing helps identify potential issues early, optimize product performance and ensure reliable quality before mass production.
Award-Winning Original Design, Custom Service, Send Us Inquiry Now
Get in Touch